HDPE or LDPE die
HDPE film is blown with a long neck above a small die; LDPE and LLDPE film with a short neck and a larger die. One line rarely does both well. Ask which resin the die was designed for.
 No Drama
Buyer guide · Plastics & molding
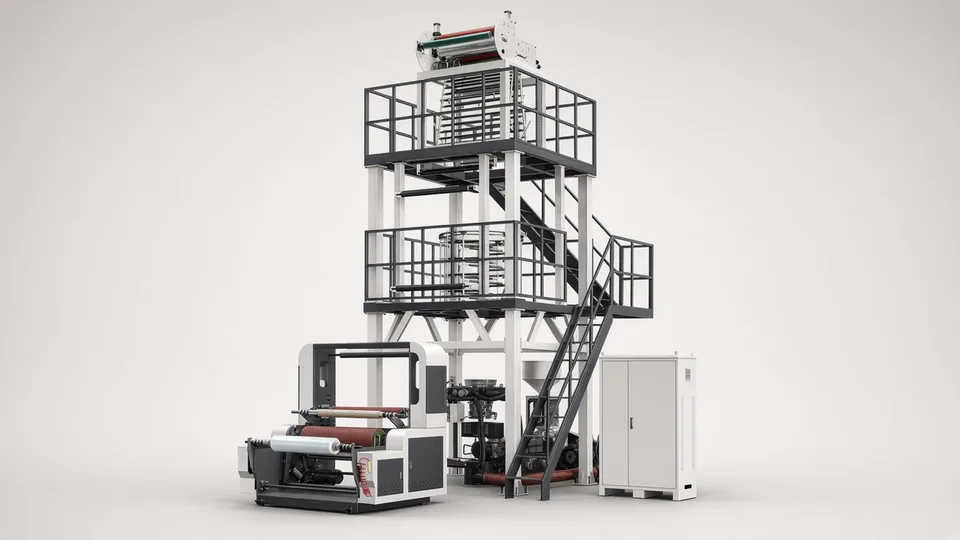
A blown film line is judged on the roll it winds, and thick and thin bands around the bubble only show when that roll is unwound on your bag or print line.
01
HDPE film is blown with a long neck above a small die; LDPE and LLDPE film with a short neck and a larger die. One line rarely does both well. Ask which resin the die was designed for.
Every die has thicker and thinner spots. Rotating the die, or oscillating the top nip, spreads them across the roll so the roll winds flat. A fixed die stacks them in one place.
A single-layer line has one extruder. An ABA line splits one extruder into outer skins; an ABC line has three separate extruders for three different recipes. Barrier film needs more layers still.
Output is limited by how fast the bubble cools. Ask whether the air ring is single or dual lip, and whether internal bubble cooling is fitted or offered as an option.
Ask for single or double winder, roll change without stopping, and whether a corona treater is included if the film will be printed.
02
Many Chinese film lines are named after the extruder: in SJ50-600, SJ is the common prefix for a single-screw extruder, 50 is the screw diameter in millimeters and 600 is the widest film the line is rated for, in millimeters. The code does not tell you output per hour; ask for that on your resin.
03
Send these with the enquiry. Without them, any number a factory gives you is a guess dressed as a quotation.
04
| Require this | A pass looks like |
|---|---|
| Run your resin at the target width and thickness until steady, then weigh output over a timed hour. | Hourly weight matches the figure in the offer for that film. |
| Measure thickness at evenly spaced points around the film. | The spread stays inside the tolerance agreed in writing before the test. |
| Unwind a full roll on a flat table. | No hard bands, wrinkles or telescoping edges. |
05
06
A plastic sheet extrusion line with a roll stack, not a bubble.
A plastic bag making machine, fed from bought rolls.
07
We name the kind of source, how many and when, and never the factory. Listed prices are asking prices, not landed cost. Where we do not hold a fact we say so: that is a GAP, not an estimate.
08
Every machine we source in this area is on the Plastics & molding page. How a project runs, stage by stage, is on how it works, and what it costs is on pricing.
Straight answers
One whose die suits your resin, with enough layers for your recipe and a rotary die if the film will be converted at speed. Compare on measured output and thickness spread.
European lines usually bring automatic gauge control and gravimetric dosing as standard. Many Chinese lines offer both as options. Price the options before comparing totals.
Die temperature zones, air ring, nip rolls, winder tension, and a timed run on your resin with output weighed and thickness measured around the film.
Usually yes. You check the Declaration of Conformity and technical file exist and match the line, and your name and address go on it.
Contact
Send a machine, a quotation you want checked, or a question. We reply with what we would look at first.
Sent
A person reads every message. You will hear back within one working day.
Not sent
Please email info@nodramachina.com directly and we will pick it up from there.