Diameter, wall and radius
Ask the tightest centreline radius at the largest diameter and your wall, in your material. A diameter alone is one third of the capacity.
 No Drama
Buyer guide · Metal & CNC
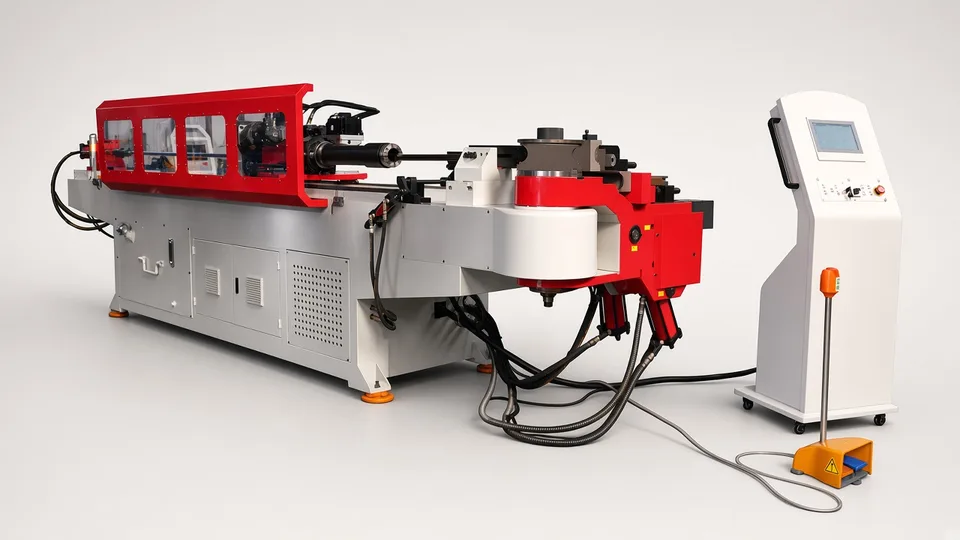
A tube bender's capacity is a diameter, a wall thickness and a bend radius together, and listings quote only the diameter, so two machines with the same number can bend very different tubes.
01
Ask the tightest centreline radius at the largest diameter and your wall, in your material. A diameter alone is one third of the capacity.
Each tube size and radius needs its own bend, clamp and pressure dies, often a wiper and mandrel too. Ask which sets are in the price.
Thin wall stainless or aluminium at a tight radius wrinkles or flattens without a mandrel and a pressure die booster. Ask whether both are fitted and driven.
A hydraulic bend arm is cheaper and strong. All servo repeats angles more easily. Ask which axes are servo: feed, rotation, bend.
A two stack head holds two radii for one part. Ask whether the software imports your XYZ or bend data, and compensates springback by material.
02
The number in codes such as DW38CNC or 89CNC is usually the largest tube outside diameter in millimetres, in mild steel. The code does not state the wall thickness or radius at that size.
03
Send these with the enquiry. Without them, any number a factory gives you is a guess dressed as a quotation.
04
| Require this | A pass looks like |
|---|---|
| After a warm-up, bend your hardest tube, thinnest wall at tightest radius, in your material. | No wrinkles inside the bend, ovality and wall thinning inside the limits on your drawing. |
| Bend ten identical parts in a row and check each on a fixture or measuring arm. | Angles and lengths repeat within your tolerance from first to tenth. |
| Enter a new part from your data file and let the software correct for springback. | Second part within tolerance after one correction cycle. |
05
06
A section or roll bender, which is a different process; four of the twenty entries were these under the same name.
An NC hydraulic bender or a used machine; CNC axes only pay back at volume.
07
We name the kind of source, how many and when, and never the factory. Listed prices are asking prices, not landed cost. Where we do not hold a fact we say so: that is a GAP, not an estimate.
08
Every machine we source in this area is on the Metal & CNC page. How a project runs, stage by stage, is on how it works, and what it costs is on pricing.
Straight answers
Servo drives and controls can match. The gap tends to be software, springback data and tooling service.
The three tests above, tooling sets counted against the order, and servo nameplates against the invoice.
A Declaration of Conformity naming its standards, the technical file behind it, and a manual in your language. A CE mark on a brochure proves nothing.
If you import it yourself, you are. You check the documents and put your name and address on the machine or its papers.
Contact
Send a machine, a quotation you want checked, or a question. We reply with what we would look at first.
Sent
A person reads every message. You will hear back within one working day.
Not sent
Please email info@nodramachina.com directly and we will pick it up from there.